Skip to content
GTRS Forged Performance Not wheels — completion of the car. 6061-T6 Forged Aluminium · Porsche-Specific Fitment
  1. Home
  2. Engineering
  3. Construction & Manufacturing

Construction & Manufacturing

From Forged Blank to Finished Wheel Set

GTRS wheels move through a controlled bespoke workflow: vehicle and fitment review, 2D/3D CAD development, structural simulation, forged 6061-T6 aluminium preparation, CNC machining, surface preparation, finishing, pre-shipment quality control, and protective export packing.

Starting Material Forged 6061-T6 Aluminium Blanks
Production Workflow 10-Stage Bespoke Sequence
Wheel Architectures Monoblock · Deep Lip · Duo-Block · Aero
Release Protocol Pre-Shipment QC Inspection & Media
CNC Machining Output · Turned & Milled 6061-T6 Stage 06 · Real Factory Media
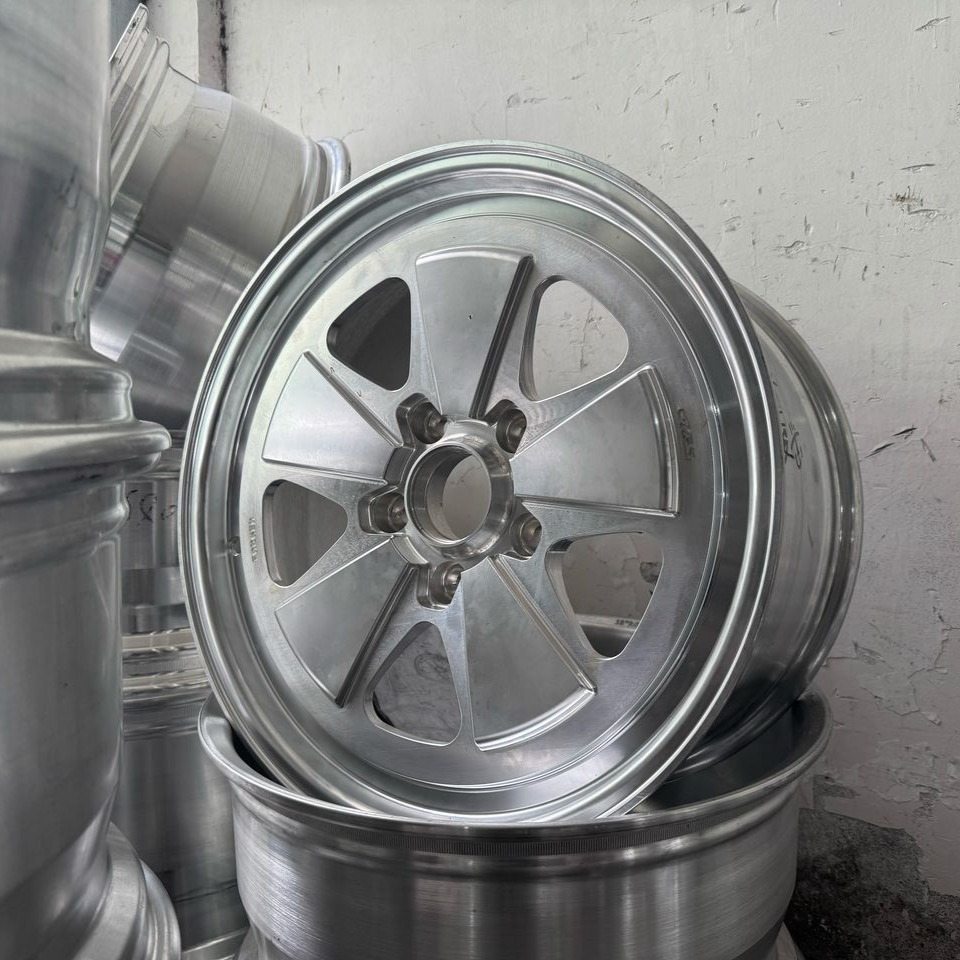
Freshly CNC-machined 5-spoke GTRS forged wheel resting on turned 6061-T6 aluminium blank

Freshly CNC-machined 5-spoke GTRS forged wheel resting directly on lathe-turned 6061-T6 aluminium blanks prior to hand surface preparation and coating.

Step-by-Step Shop-Floor Sequence

How a Bespoke GTRS Wheel Set Is Engineered, Machined, and Inspected

Rather than pulling pre-cast wheels from warehouse shelving, every GTRS order progresses sequentially from vehicle-specific CAD and structural validation to forged 6061-T6 blank turning, multi-axis CNC milling, hand surface preparation, finishing, and documented pre-shipment quality control.

Stage 01 Engineering Input Pre-Machining Engineering

Vehicle & Fitment Specification

Every wheel set begins with vehicle platform verification, wheel construction selection, and target fitment parameters before any CAD solid or machining toolpath is generated. Front and rear axle requirements are defined independently so staggered widths, offset targets, and brake envelopes match the chassis configuration.

Key Checks

  • Vehicle model, generation, and suspension/brake setup review
  • Front and rear diameter, width, and offset (ET) target confirmation
  • Bolt pattern (PCD), center bore, and lug hardware seat specification
  • Construction family selection (Monoblock, Monoblock Deep Lip, Duo-Block, or Aero)
Engineering Input Stage 01 · Fitment Plate
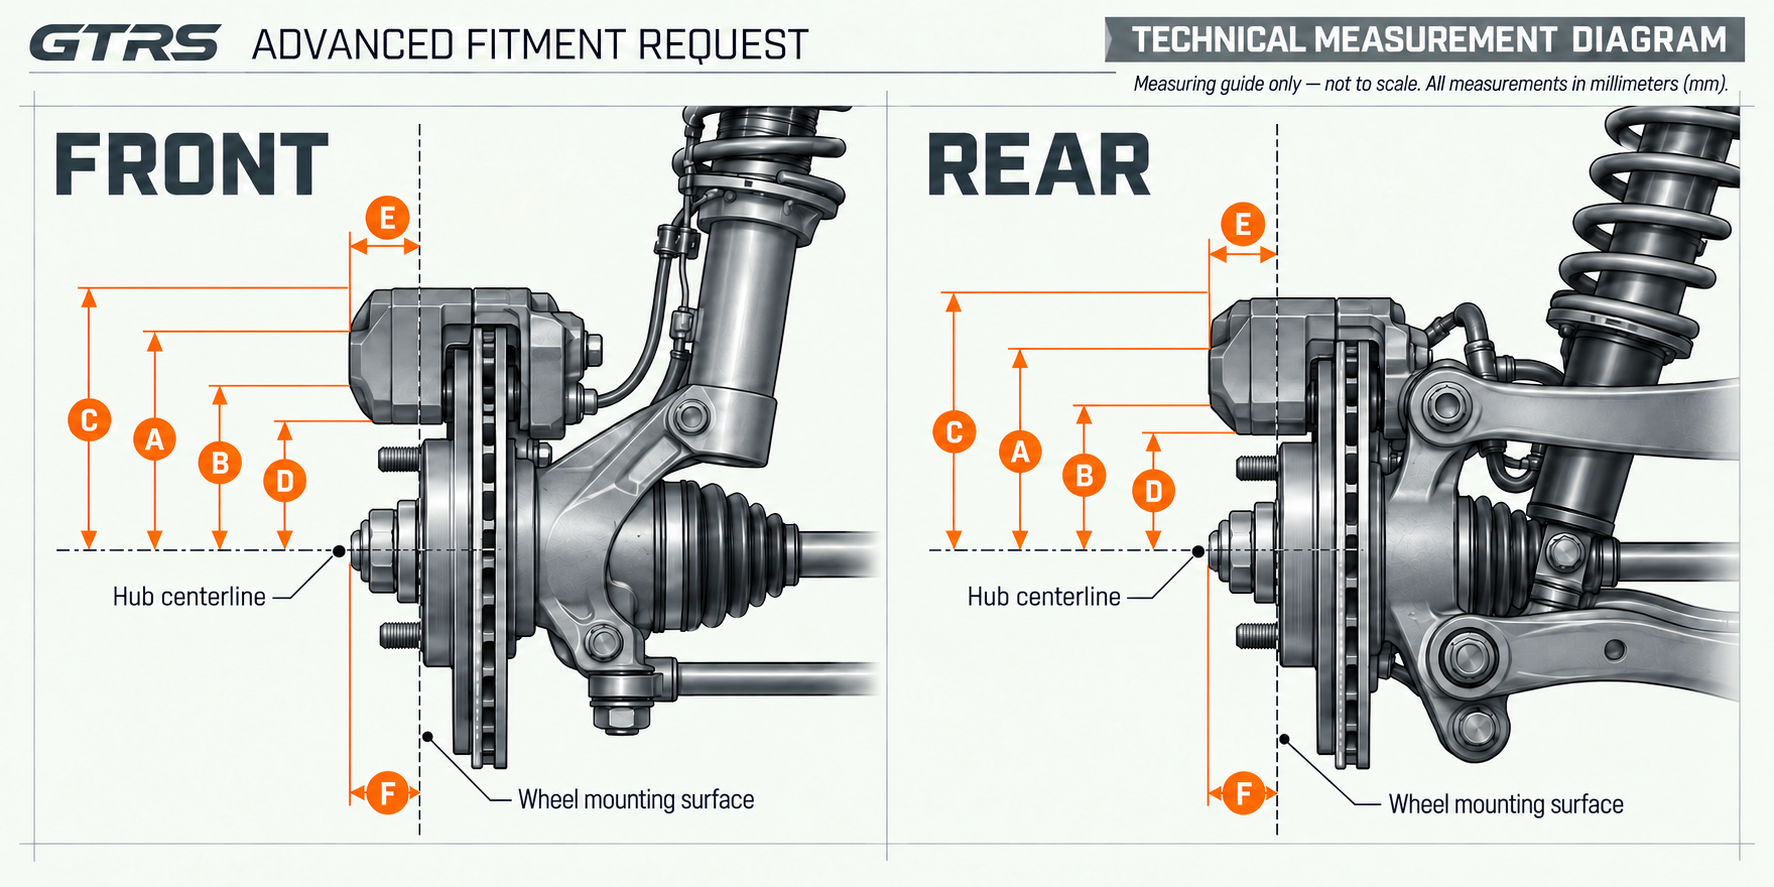
Detailed FRONT and REAR brake and hub measurement guide with A–F arrows. All values in millimeters; not to scale.

Front and rear staggered fitment architecture defining rim width, offset (ET), center bore, and brake-clearance envelope prior to CAD modeling.
Stage 02 CAD Development Pre-Machining Engineering

2D / 3D CAD Wheel Architecture

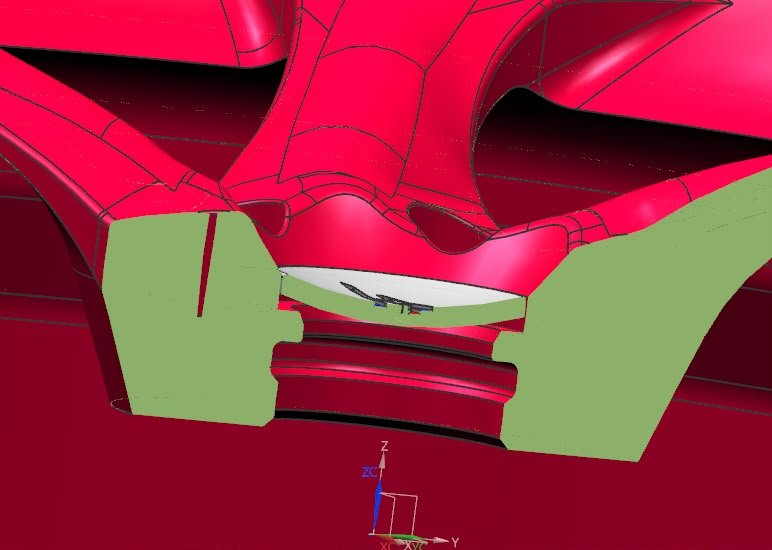
Once the fitment envelope is locked, 2D cross-sections and 3D solid CAD models define spoke profile, concave depth, outer lip step, mounting pad thickness, and inner barrel contour. Horizontal section cuts verify center-bore steps, lug-pocket counterbores, and machined center-cap retention interfaces before structural review.

Key Operations

  • 2D radial and horizontal cross-section layout for hub pad, center bore, and cap retention
  • 3D solid modeling of spoke geometry, window reliefs, and front/rear concavity differential
  • Brake caliper sweep and rotor-hat plane clearance verification inside the 3D profile
  • Customer 3D design and specification sign-off prior to blank turning and CNC programming
CAD Development Stage 02 · 2D/3D CAD Cross-Section
2D/3D CAD cross-section of center bore, mounting pad step, and machined center cap interface

Horizontal CAD section profile detailing center-bore step geometry, hub mounting face, and custom-machined center cap interface.

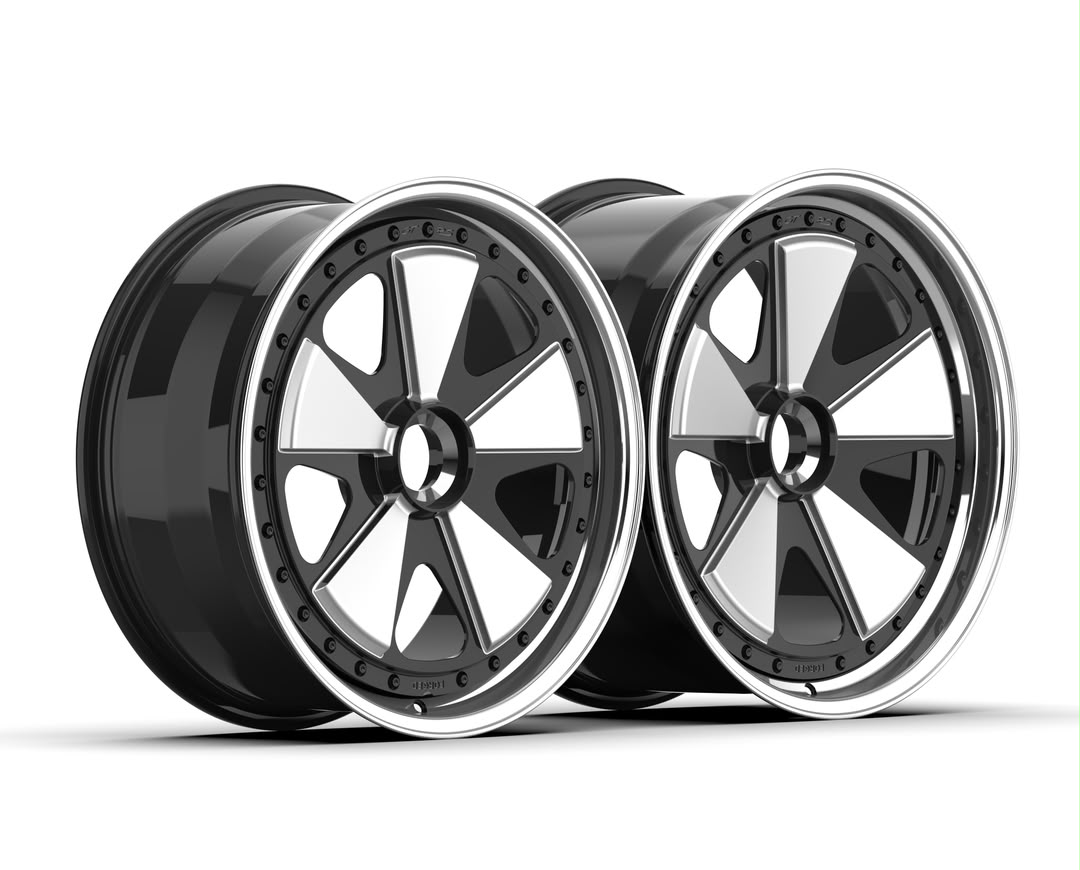
GTRS 3D CAD front and rear wheel solid geometry render
3D Solid Assembly Front and rear 3D CAD wheel models verifying staggered spoke depth and barrel geometry.
Stage 03 Digital Validation Pre-Machining Engineering

Structural & Load Simulation

Before releasing a bespoke wheel geometry to CNC production, digital Finite Element Analysis (FEA) evaluates how loads travel through the spokes, spoke-to-rim junctions, and mounting pad. Stress contour mapping allows engineers to refine pocket radii and section thickness while keeping unsprung mass controlled.

Key Checks

  • Digital stress distribution analysis across spoke roots, window fillets, and hub mounting pad
  • Evaluation of cornering, radial, and impact load paths within the 3D CAD solid model
  • Refinement of spoke back-pocketing depth and transition radii before CAM toolpath lock
  • Verification of structural geometry for the vehicle axle load context prior to machining
Digital Validation Watch FEA Simulation · 12s

Representative FEA simulation · 12 seconds · No audio. Colour contours show the simulated stress distribution across the wheel.

Stage 04 Raw Forged Blank Material & Blank Preparation

Forged 6061-T6 Aluminium Starting Material

Physical production starts with dense forged 6061-T6 aluminium starting blanks rather than cast liquid metal poured into a mold. Each cylindrical blank is selected according to the target wheel diameter, width, concavity depth, and construction family (single-piece Monoblock blank or dedicated Duo-Block center disc and barrel stock).

Key Checks

  • Forged 6061-T6 aluminium alloy starting blank selection matched to wheel diameter and width
  • Visual and dimensional receiving inspection of raw cylindrical forgings before chucking
  • Separation of single-piece full-width blanks and two-piece center-disc forging stock
  • Batch identification and routing to lathe turning according to order specification
Raw Forged Blank Stage 04 · Raw 6061-T6 Stock
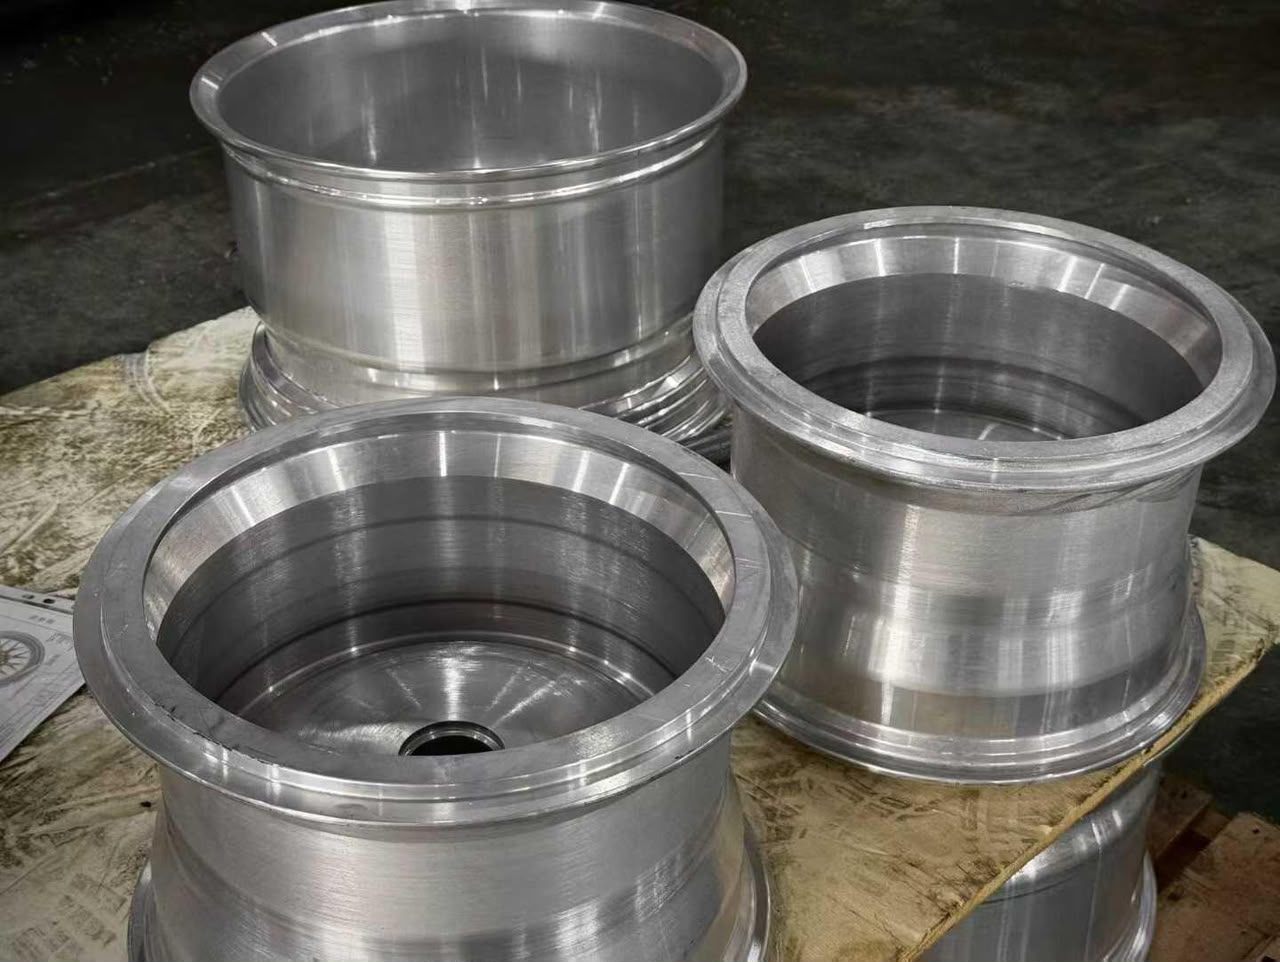
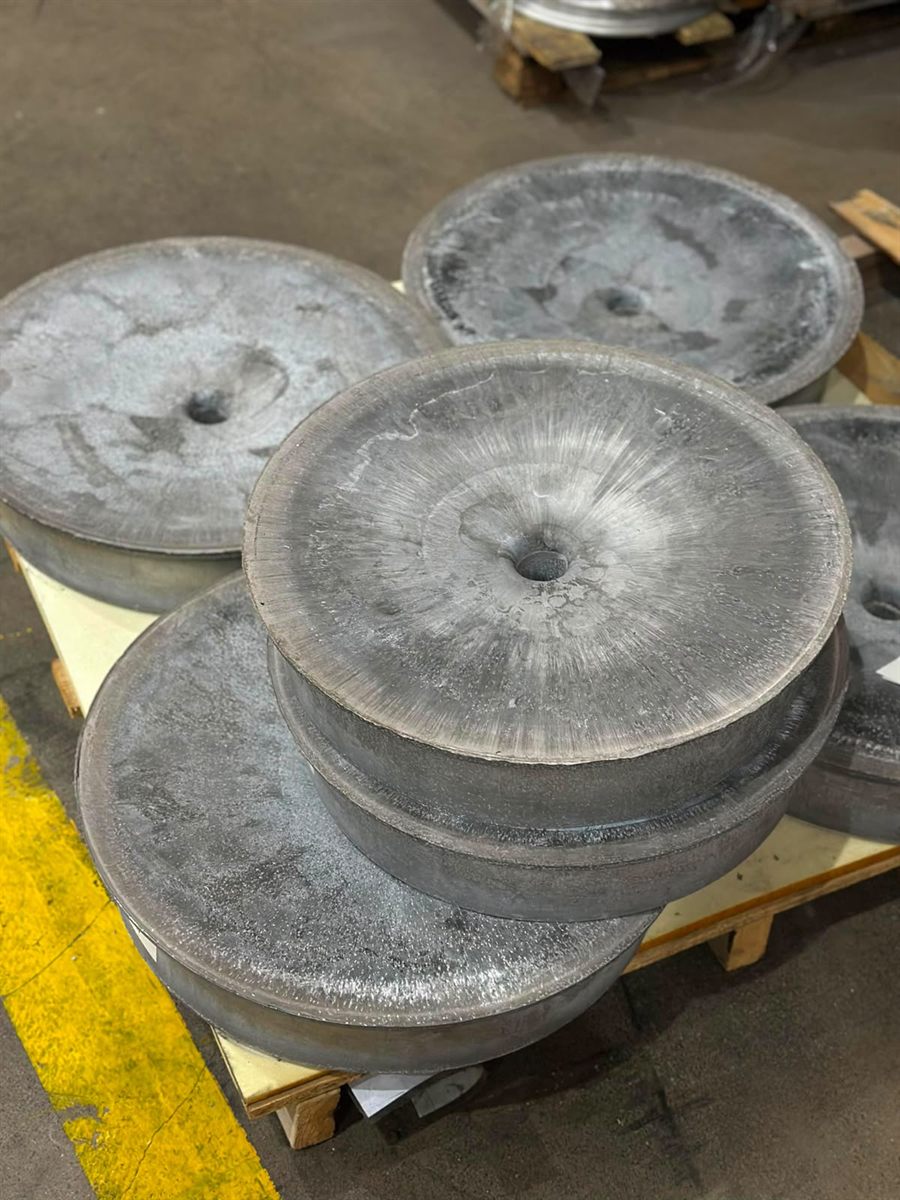
Stacked forged 6061-T6 aluminium cylindrical starting blanks prior to lathe turning

Raw forged 6061-T6 aluminium starting blanks staged on the production floor prior to initial lathe turning and face profiling.

Stage 05 Lathe Profiling Material & Blank Preparation

Blank Preparation & Turning

On heavy-duty CNC lathes, the raw forged blank is turned into an axisymmetric pre-milling blank. This stage establishes the outer rim lip contour, tire bead seats, inner barrel profile, rear hub mounting pad, and front face concavity curve—creating the exact rotational envelope that CNC milling will subsequently sculpt.

Key Operations

  • Lathe turning of the front concave or deep-lip profile according to the approved 2D/3D CAD section
  • Machining of inner and outer tire bead seats, rim flanges, and barrel wall contour
  • Turning of the rear hub mounting pad plane and inner brake-clearance sweep
  • Establishment of concentric reference datums for multi-axis CNC milling fixturing
Lathe Profiling Stage 05 · Turned Pre-Milling Blanks
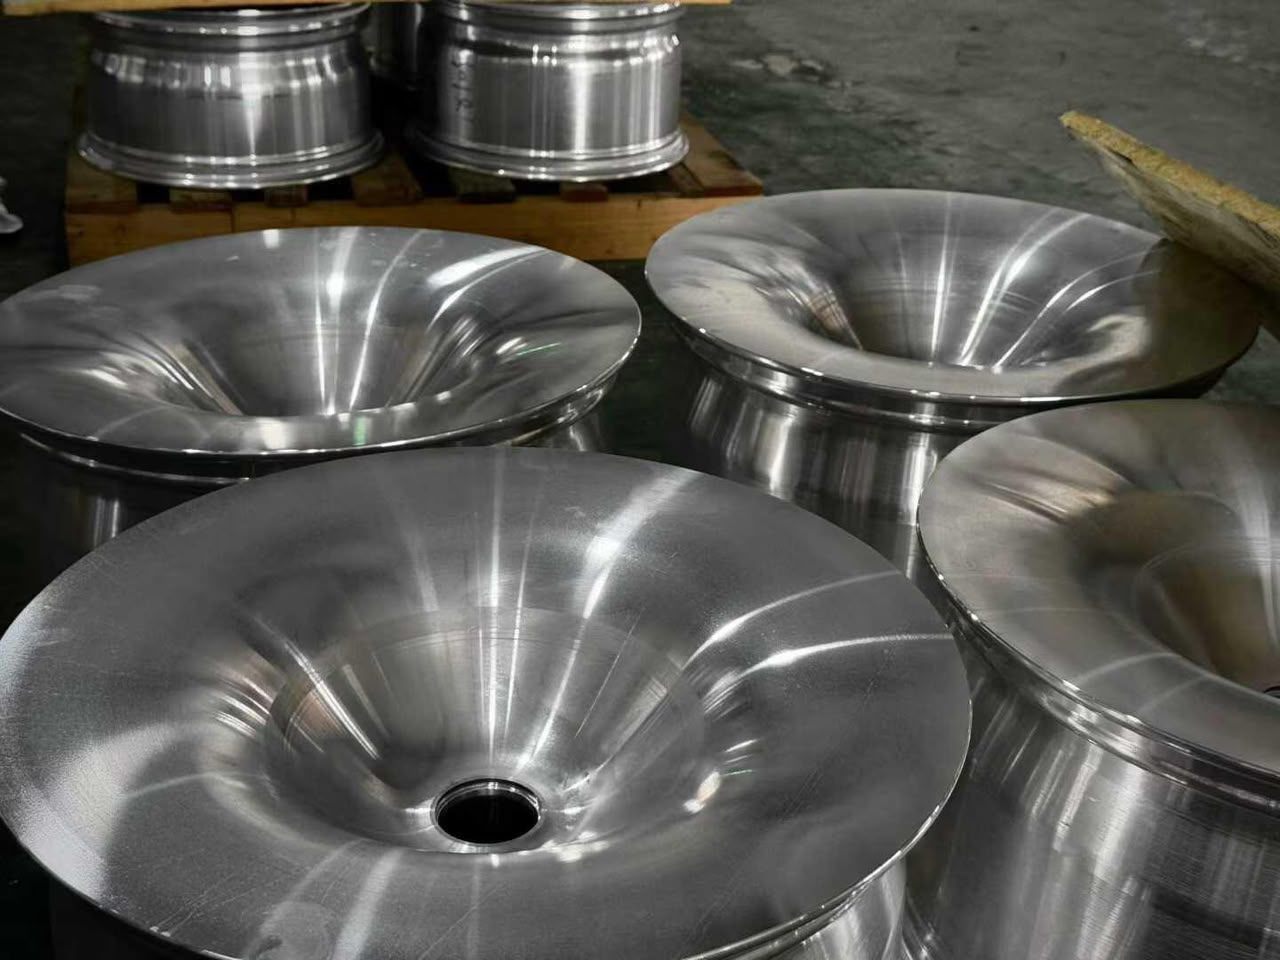
Four lathe-turned 6061-T6 forged wheel blanks with deep concave face contours ready for CNC milling

Lathe-turned 6061-T6 forged blanks with pre-profiled deep-concave face contours and rim flanges ready for CNC spoke milling.

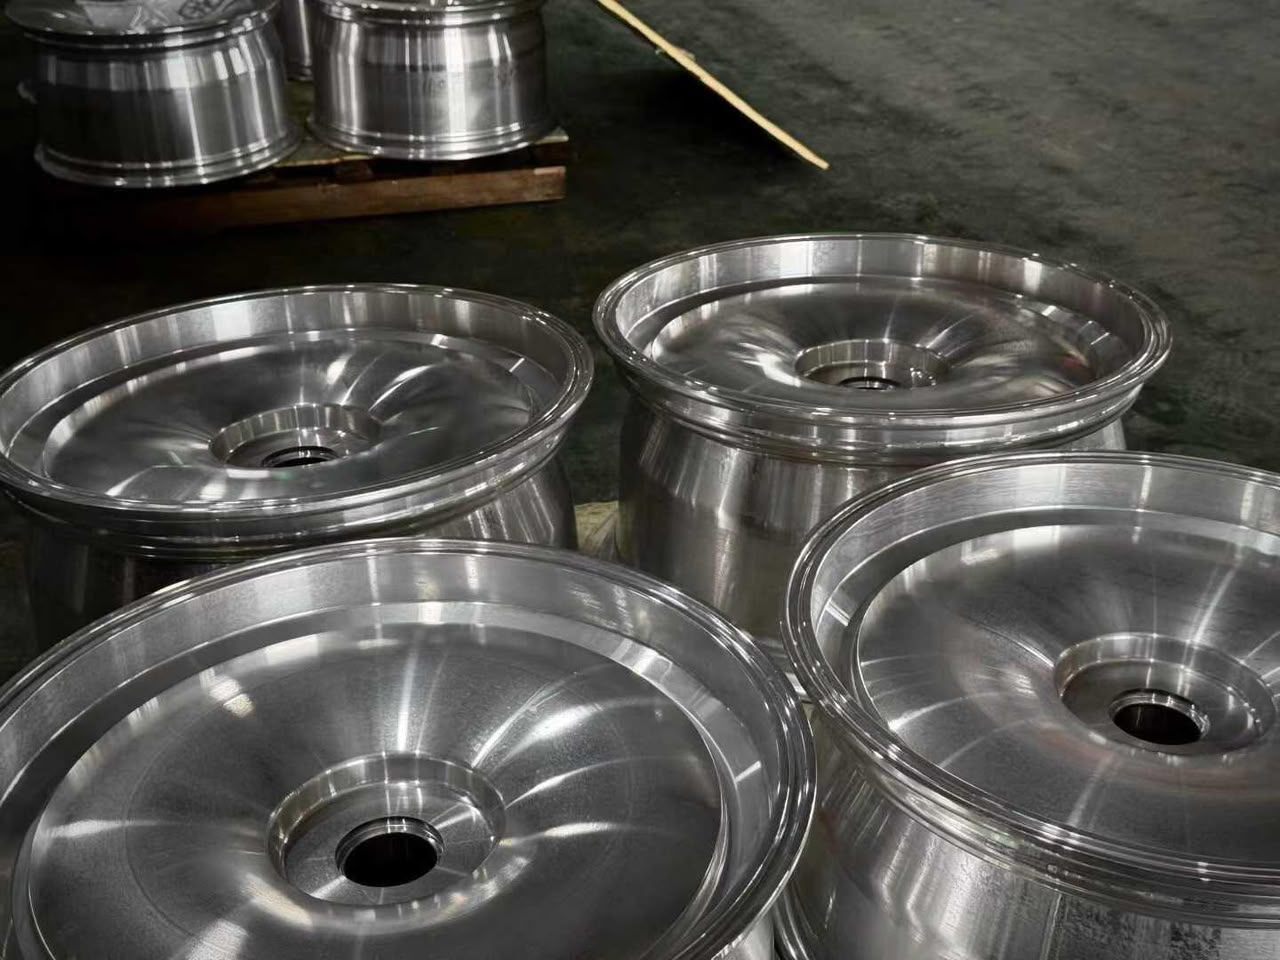
Rear mounting pad and inner barrel contour on lathe-turned forged blanks prior to milling
Backpad & Inner Rim Rear mounting pad and inner barrel contour turned prior to spoke window milling.
Four lathe-turned 6061-T6 forged blanks with integrated deep-lip outer flange profiles
Deep Lip Blank Profile Turned Monoblock Deep Lip blanks with integral stepped outer rim lip geometry.
Stage 06 Multi-Axis Milling Precision Machining

CNC Machining

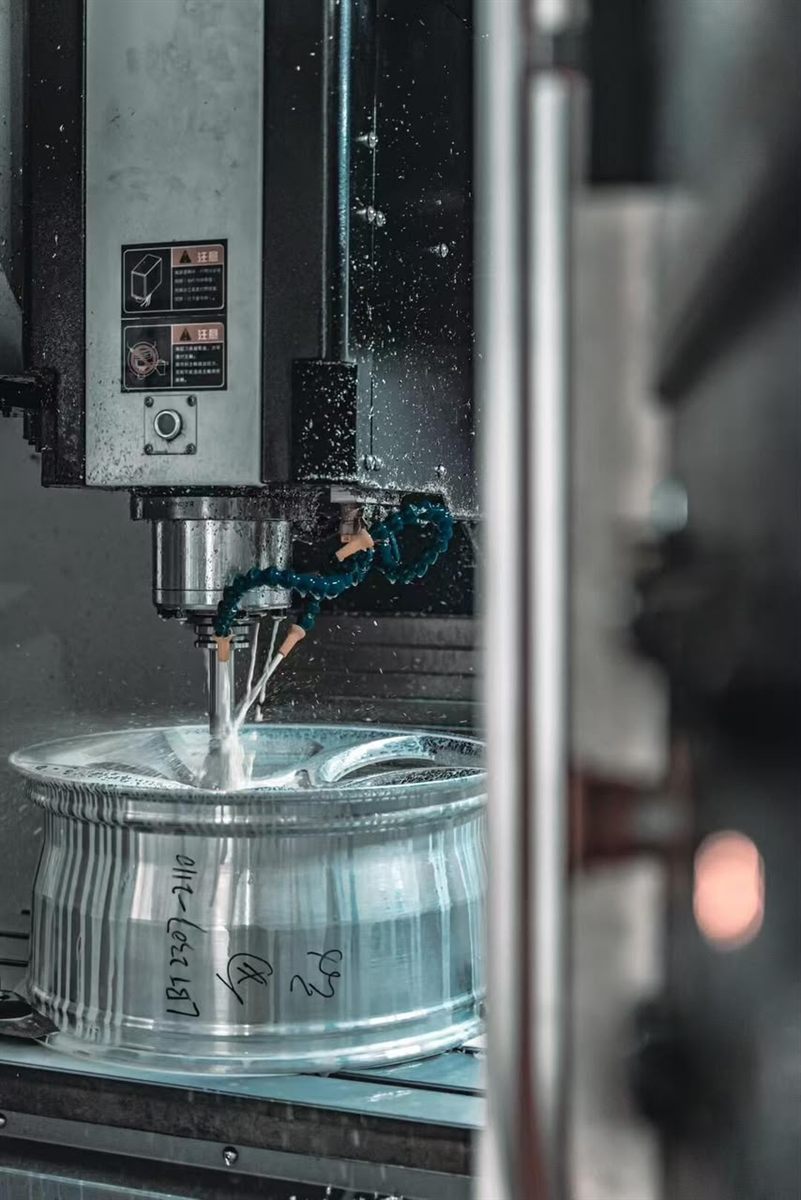
The turned blank is clamped onto the CNC machining bed where high-speed tooling carves the spoke windows, spoke side-cuts, weight-reduction back pockets, lug bolt holes, center bore, and cap register under continuous coolant flow. Rim lip specification markings and brand engravings are machined directly into the metal.

Key Operations

  • First-stage rotary bed fixturing and datum probing on center bore and mounting pad
  • Roughing and fine-step finishing of spoke windows, chamfers, and three-dimensional spoke sculpting
  • Precision boring of vehicle-specific hub-centric center bore, PCD bolt holes, and valve stem port
  • Direct CNC engraving of wheel specification markings and GTRS rim-lip identification
Multi-Axis Milling Watch CNC Milling · 16s

Watch the cutter shape the wheel spokes under continuous coolant flow. Workshop footage · 16 seconds · No audio.

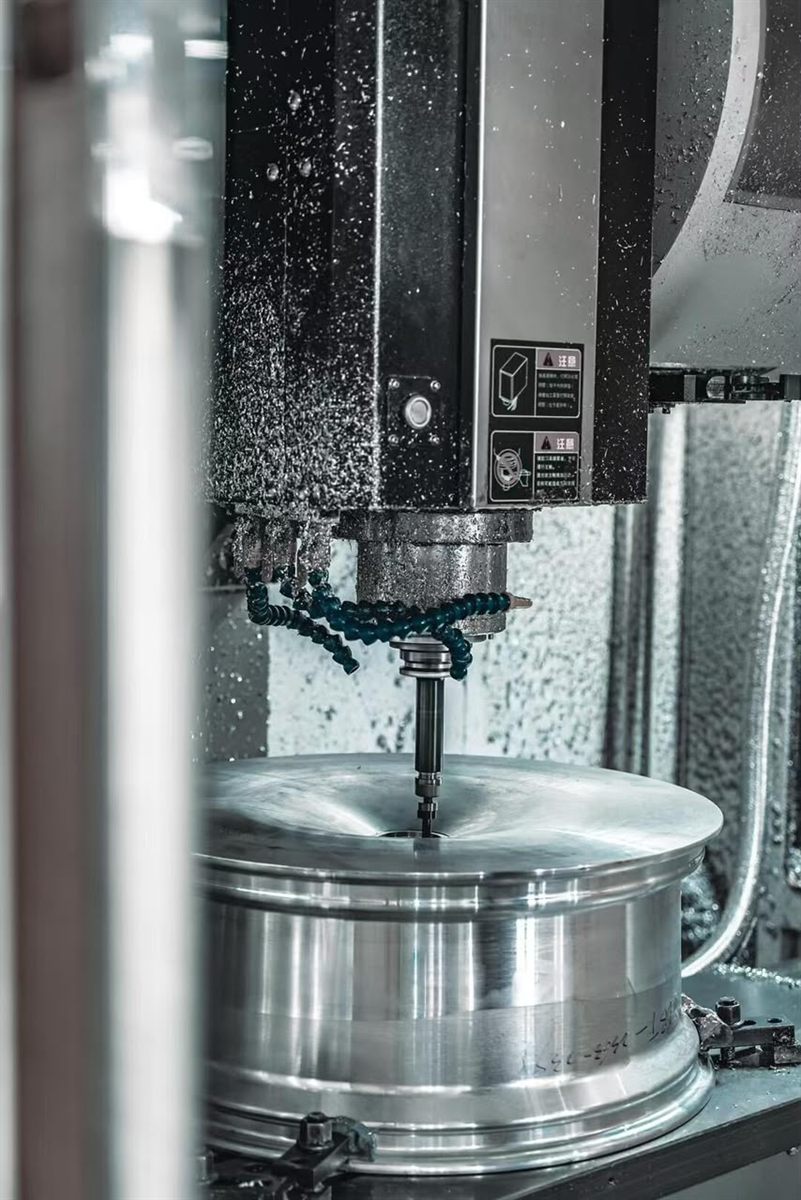
Turned forged aluminium blank clamped on CNC rotary bed with spindle and coolant nozzles
First-Stage Fixturing Turned blank clamped on CNC table establishing center-bore and lug-seat datums.
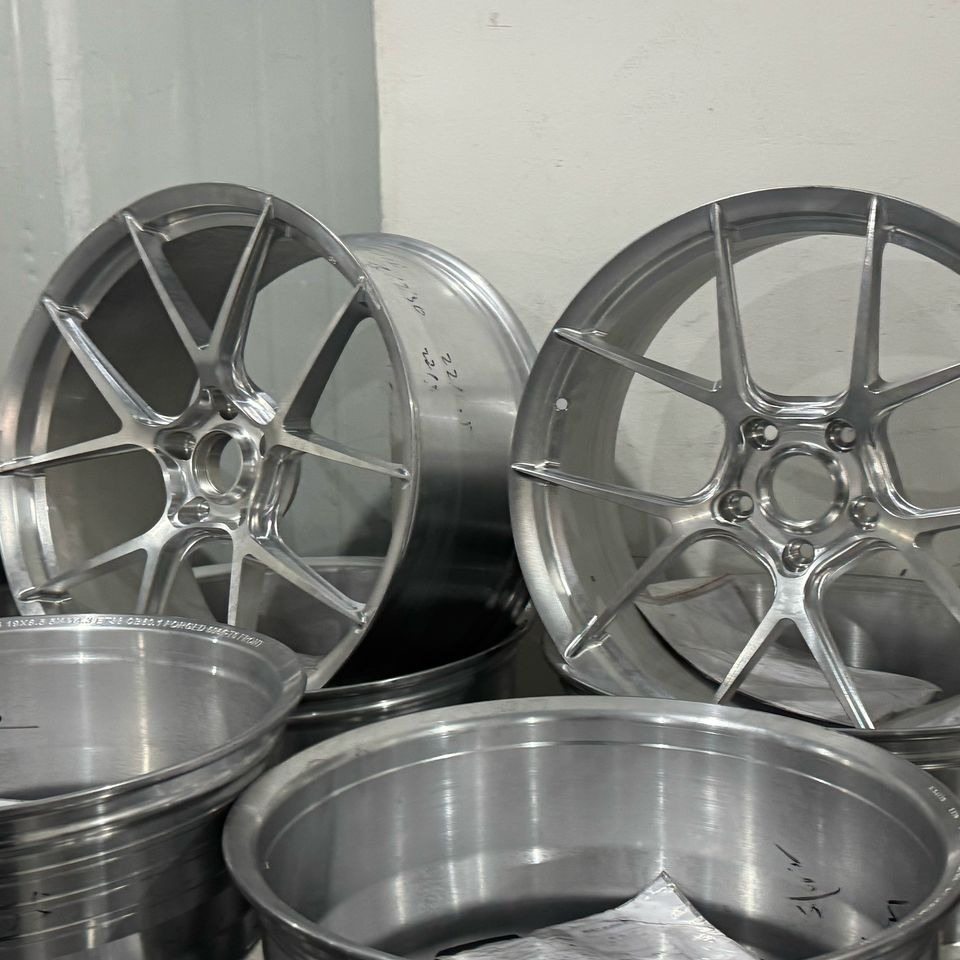
Two freshly CNC-machined split-5-spoke GTRS forged wheels resting on turned blanks
Post-Milling Output Freshly milled split-5-spoke forged wheels resting on turned blanks after CNC release.
Stage 07 Hand Preparation Surface & Coating

Surface Preparation

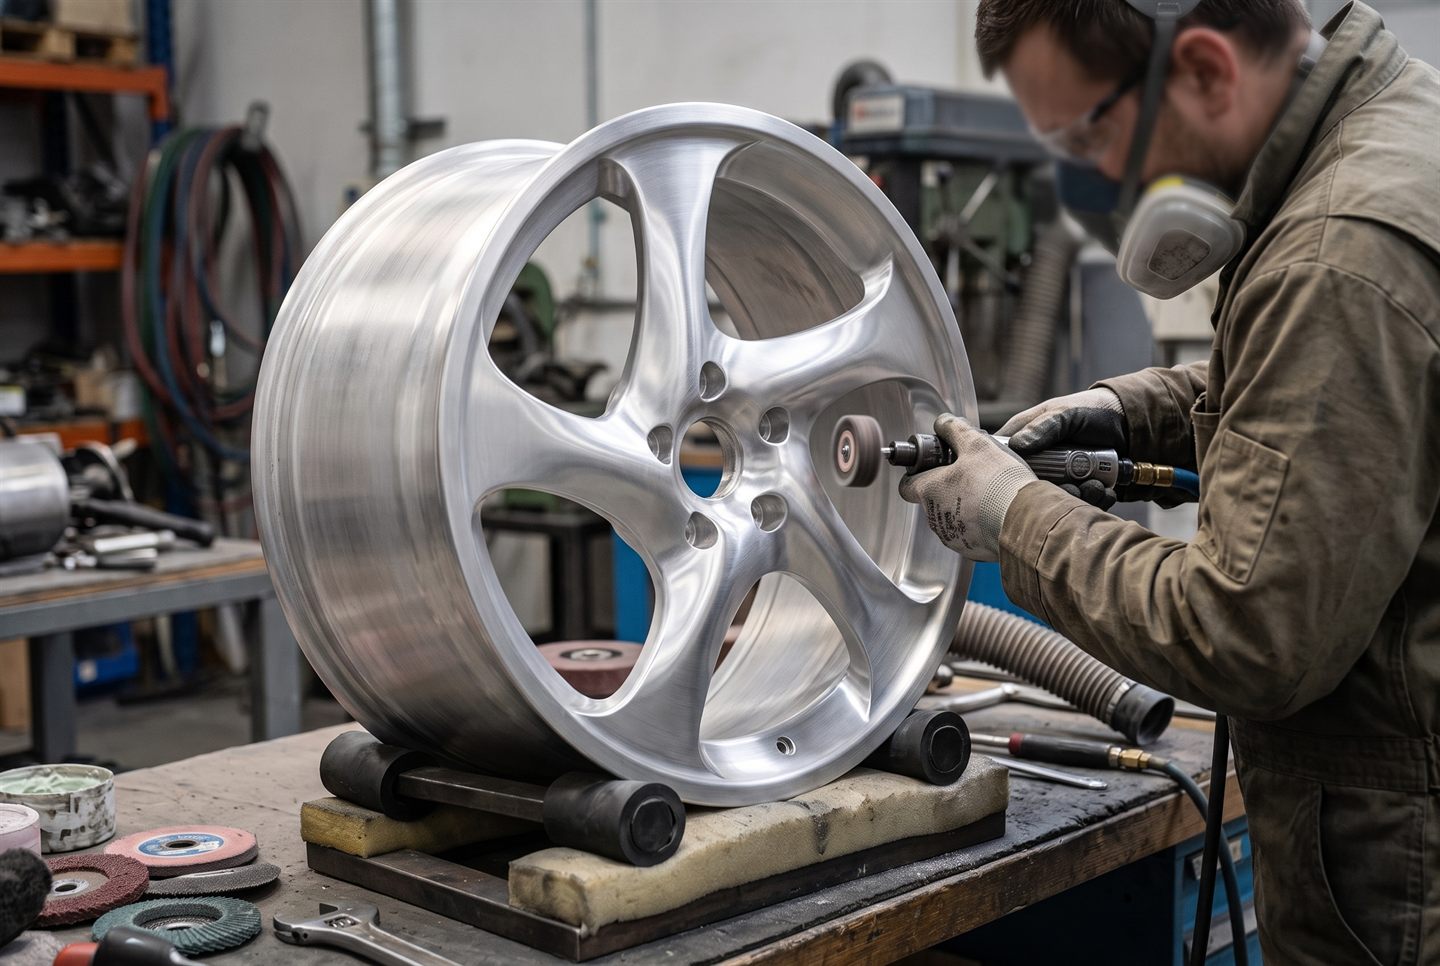
When a wheel leaves the CNC mill, every spoke edge, lug pocket, and window transition undergoes manual deburring and progressive surface conditioning. Because thin-film powder coats, brushed clears, and mirror polishes reveal every underlying substrate mark, hand preparation defines the clarity of the final finish.

Key Operations

  • Manual deburring of CNC tool exits around spoke windows, lug counterbores, and rear pockets
  • Progressive abrasive smoothing across spoke faces, window walls, and outer lip transitions
  • Dedicated directional brushing or multi-stage mechanical polishing for transparent finish families
  • Chemical degreasing and surface cleaning prior to primer, powder, or clear-coat application
Hand Preparation Stage 07 · Manual Pocket Prep
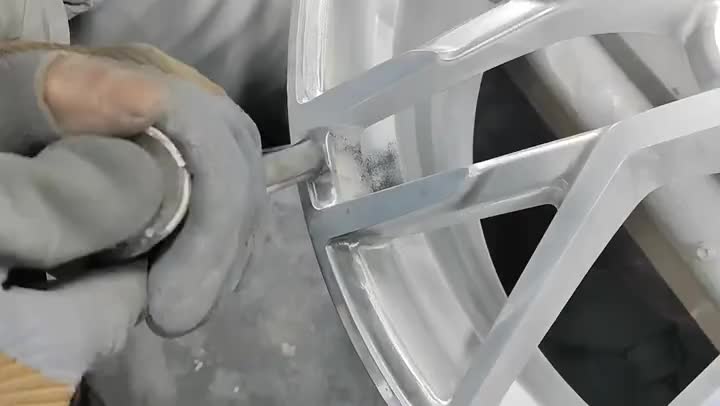
Technician performing manual deburring and surface preparation inside a machined spoke pocket

Gloved technician performing manual deburring and surface refinement inside a CNC-machined spoke pocket.

Hand surface preparation and fine conditioning across machined forged wheel spokes
Spoke Face Conditioning Fine-grit surface preparation across spoke faces and rim flange prior to coating.
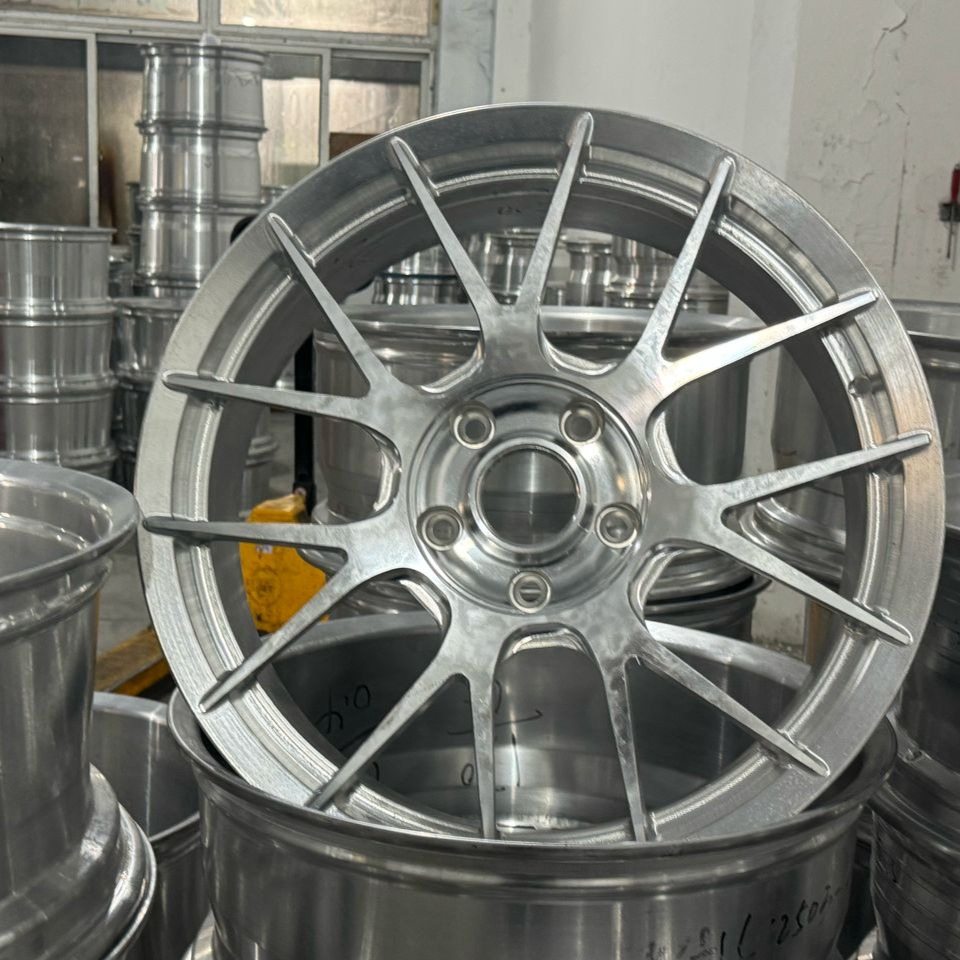
Freshly CNC-machined twin-spoke GTRS forged wheel surrounded by stacked aluminium blanks
Raw Machined Substrate Raw CNC-machined twin-spoke wheel inspected for pocket edge uniformity before hand prep.
Stage 08 Coating & Clearcoat Surface & Coating

Finishing & Coating

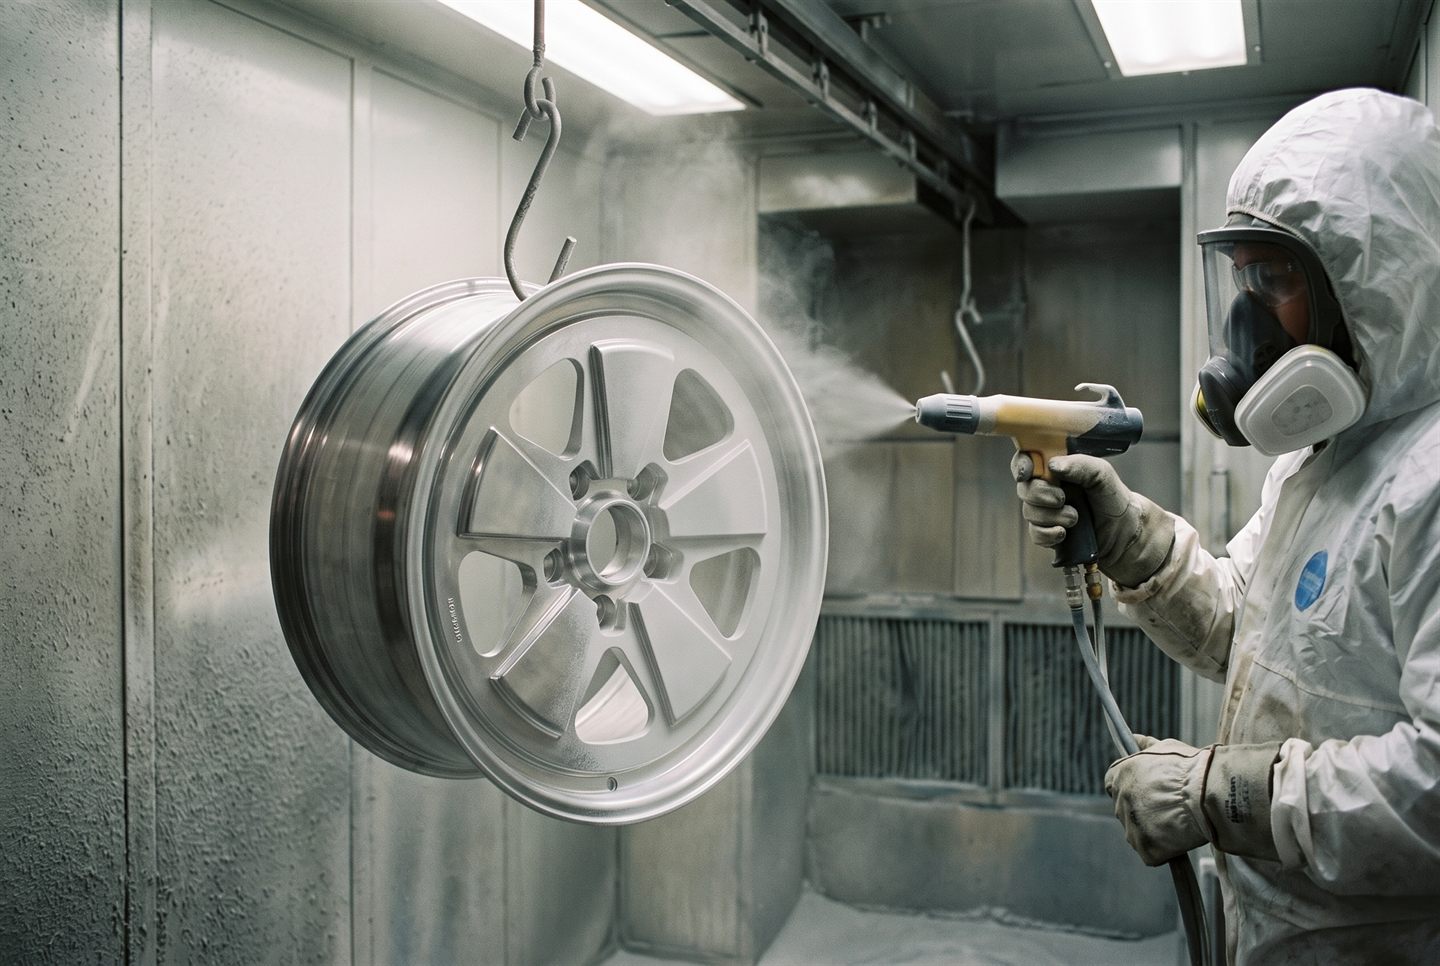
Prepared wheels move into controlled finishing booths where the selected GTRS finish architecture is applied—ranging from solid and metallic powder coats to tinted transparent clears over brushed or polished aluminium, precision diamond-cut face machining, or independent center-and-barrel two-piece contrast finishes.

Key Operations

  • Masking of hub mounting pad, center-bore register, and tapered/ball lug seats to preserve bare metal
  • Controlled application of powder coat, liquid metallic color, or tinted/clear protective topcoat
  • Thermal curing cycle and film-uniformity check across deep spoke windows and inner barrel walls
  • Independent finishing of center disc and barrel components on two-piece Duo-Block builds prior to assembly
Coating & Clearcoat Stage 08 · Spray Booth Application
Controlled spray-booth finish application on a suspended 5-spoke forged wheel

Controlled spray-booth finish and protective clearcoat application on a suspended 5-spoke forged wheel.

Stage 09 Pre-Shipment QC Inspection & Dispatch

Quality-Control Inspection

Before any wheel set is cleared for packing, all four wheels are staged together for final quality control. Technicians verify fitment specifications, mounting geometry, center cap fit, and surface finish continuity across the complete front and rear set, recording pre-shipment inspection photography for order documentation.

Key Checks

  • Verification of diameter, width, offset (ET), bolt pattern (PCD), and center bore against order sheet
  • Inspection of bare-metal hub mounting pad cleanliness, lug seat finish, and center cap seating
  • Full-set visual inspection of finish tone, gloss/satin consistency, and inner barrel cleanliness
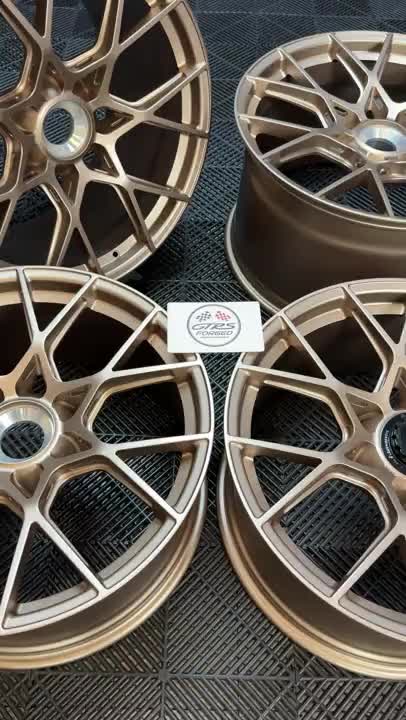
  • Capture of pre-shipment QC photography and video confirmation with the GTRS inspection placard
Pre-Shipment QC Watch Final QC · 30s

Final visual inspection of a Satin Neodyme Gold GTRS wheel set before dispatch. Workshop footage · 30 seconds · No audio.

Stage 10 Protective Export Packing Inspection & Dispatch

Packing & Dispatch

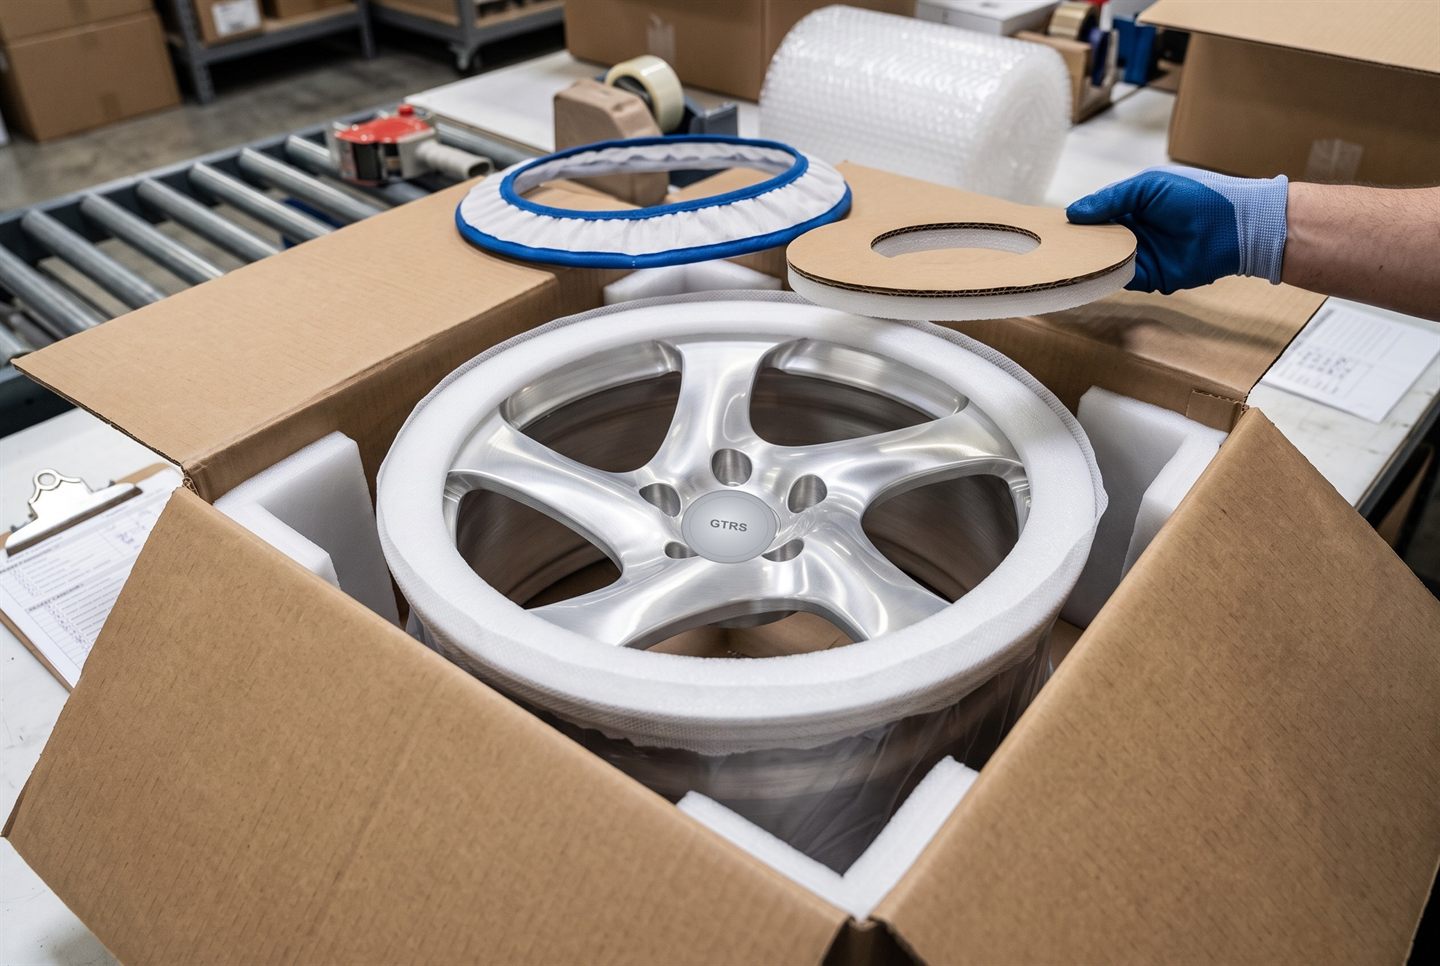
Approved wheels are individually wrapped and cradled inside heavy-wall export cartons for international courier and freight transit. Perimeter rim guards, dense foam collars, and face protection sheets isolate the finished surfaces from vibration or impact between the production floor and the customer or installing workshop.

Key Operations

  • Installation of protective face cover, outer rim flange guard ring, and fitted perimeter foam cradle
  • Placement of matching center caps and order identification labeling per front/rear axle position
  • Sealing inside reinforced individual wheel cartons engineered for international parcel and pallet transit
  • Dispatch handoff with shipment tracking documentation provided to the customer or workshop
Protective Export Packing Stage 10 · Export Carton Protection
Finished GTRS forged wheel protected by perimeter foam collar and rim guard inside export carton

Finished GTRS forged wheel cradled in high-density perimeter foam and rim flange protection inside an individual export carton.

Construction-Specific Manufacturing

How Blank Turning, CNC Milling, and Assembly Adapt Across the 4 Architectures

While every GTRS wheel begins with forged 6061-T6 aluminium and vehicle-specific CAD engineering, lathe profiling, spoke milling depth, finishing workflows, and final assembly differ across the four wheel construction families.

Architecture 01 · Single-Piece Forging

Monoblock

1-Piece 6061-T6
Four lathe-turned 6061-T6 forged wheel blanks with deep concave face contours ready for CNC milling

One-piece forged construction machined from a single 6061-T6 blank for balanced stiffness, clean load path, and everyday/performance versatility.

  • Turned on a single continuous concave face and barrel blank profile
  • Spoke windows, side-cuts, and backpad weight pockets milled in one monolithic piece
  • Zero perimeter assembly hardware for clean maintenance and direct spoke-to-rim stiffness
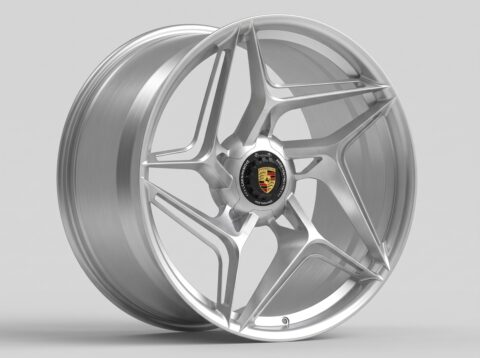
Forged Wheel GTRS - F.F42
Representative Model Forged Wheel GTRS - F.F42
Inspect Model
Architecture 02 · Stepped Outer Rim Profile

Monoblock Deep Lip

1-Piece Deep Lip
Four lathe-turned 6061-T6 forged blanks with integrated deep-lip outer flange profiles

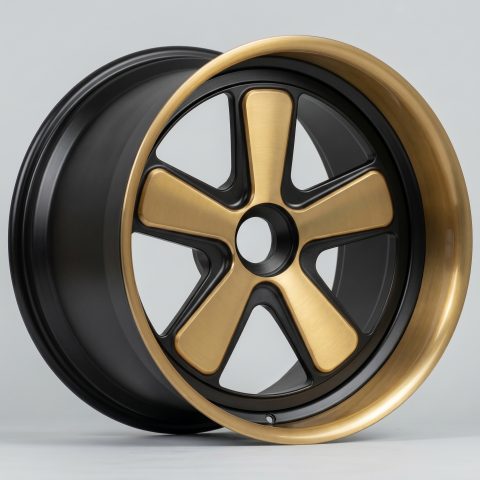
Single-piece architecture with deeper outer lip profile and deeper visual step while retaining one-piece structural continuity.

  • Lathe-turned with a recessed spoke mounting plane and integral deep outer lip shelf
  • Retains one-piece structural continuity without multi-piece sealing joints
  • Supports two-tone machined/polished outer lip and coated center transitions on a single forging
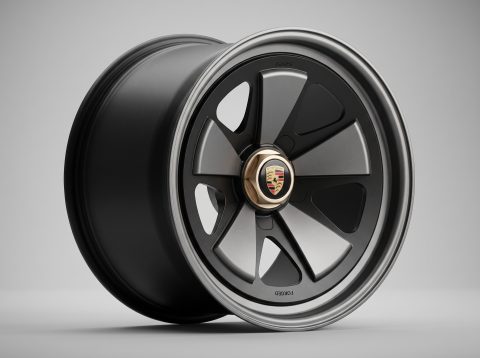
Forged Wheel GTRS – P.F993S
Representative Model Forged Wheel GTRS – P.F993S
Inspect Model
Architecture 03 · Two-Piece Modular Assembly

Duo-Block

2-Piece Modular
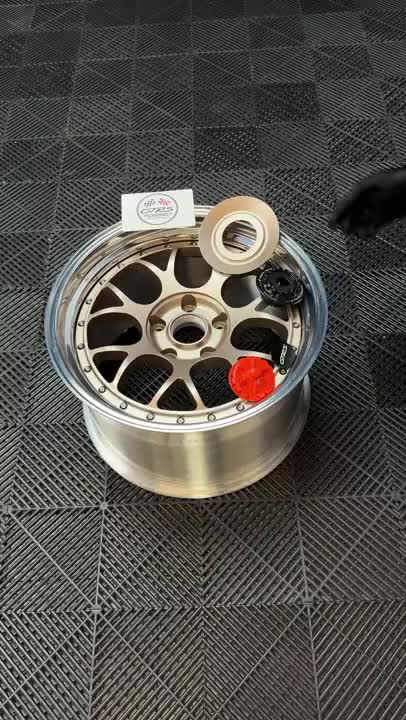
Two-piece Duo-Block forged wheel rim and center disc hardware assembly inspection

Two-piece modular construction separating center and barrel for broader width/offset flexibility and multi-piece finish combinations.

  • Forged center disc and rim barrel machined and finished as independent components
  • Allows independent powder coat, brushed, or polished treatments on center and outer lip
  • Precision perimeter hardware assembly with concentricity verification before QC sign-off
Forged Wheel GTRS - P. 0930FCH
Representative Model Forged Wheel GTRS - P. 0930FCH
Inspect Model
Architecture 04 · Monoblock Construction · Aero Design Family

Aero

Design Family: Aero
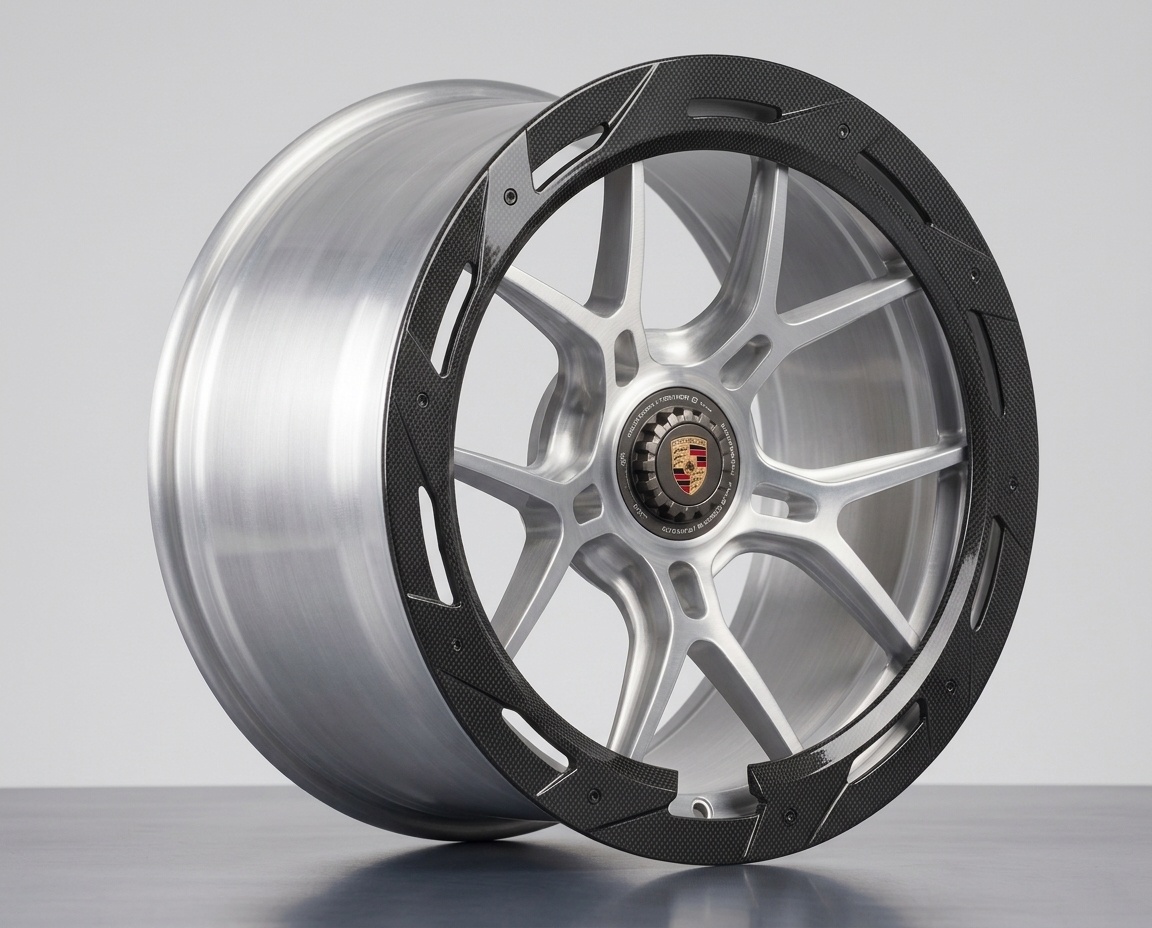
GTRS P.AERO 089 — Monoblock construction with Aero Design Family in Brushed Clear

Remains Monoblock construction with an Aero Design Family—machined from a single 6061-T6 forging with precision outer aerodynamic ring/disc integration.

  • Construction: Monoblock
  • Design Family: Aero
  • Precision-machined outer aerodynamic ring/disc profile verified on GTRS P.AERO 089
Forged Wheel GTRS – P. AER 089
Representative Model Forged Wheel GTRS – P. AER 089
Inspect Model

Material & Machining Discipline

Forged 6061-T6 Aluminium Condition vs. Machined Wheel Architecture

In bespoke wheel manufacturing, material specification and structural architecture describe two distinct layers of the build: `6061-T6` defines the forged aluminium starting alloy and thermal temper condition, while the construction family defines the mechanical geometry sculpted from that blank.

01 · Material Condition

What 6061-T6 Forged Aluminium Means

`6061` designates a wrought aluminium-magnesium-silicon alloy, and `-T6` designates solution heat-treating followed by artificial aging. Starting from a dense solid forged blank rather than a gravity or low-pressure casting provides a uniform wrought substrate for high-detail CNC milling.

  • Solid wrought forging stock free from casting porosity pockets
  • Consistent machinability across thin spoke webs and deep pockets
  • Clean substrate for transparent brushed and mirror-polished finishes
02 · Structural Architecture

Material Condition vs. Wheel Geometry

Every GTRS construction—`Monoblock`, `Monoblock Deep Lip`, `Duo-Block`, and `Aero`—shares the same forged 6061-T6 aluminium material foundation. What changes between families is how the blank is turned, whether the center and barrel are monolithic or modular, and how outer ring geometry is integrated.

  • Monoblock & Deep Lip: machined from a single full-width forging
  • Duo-Block: independent forged center disc and barrel assembly
  • Aero: precision-machined outer aerodynamic ring integration
03 · Mounting Precision

Why CNC Machining Precision Matters on the Hub

The center bore and hub-contact surfaces are machined according to the approved vehicle-specific specification to support accurate centering and mounting.

  • Direct hub-centric center bore sizing matched to the vehicle hub register
  • Vehicle-specific bolt circle (PCD) and lug seat geometry machined per order
  • Bare-metal hub mounting pad masked during coating for clean hub-face contact

Downstream Surface Architecture

How CNC Machining and Hand Prep Feed the 5 GTRS Finish Families

Stages 07 and 08 of the manufacturing sequence adapt directly to the chosen finish family. Opaque powder coats, transparent brushed clears, mirror polishes, diamond-cut faces, and two-piece contrast builds each require a dedicated substrate preparation path before coating.

Family 01

Standard Powder Coat

Thermally cured solid and metallic powder coatings applied over chemically prepped CNC-machined surfaces for durable all-season protection.

Satin Black · Gloss Silver · Dark Graphite · Aurum
Family 02

Brushed

Directional hand and machine-brushed 6061-T6 aluminium grain sealed beneath clear or tinted transparent topcoats that showcase raw machining lines.

Brushed Clear · Brushed Gold · Brushed Turbonite
Family 03

Polished

Multi-stage mechanical polishing that brings the dense forged aluminium substrate to a high-clarity mirror luster before protective sealing.

Full Mirror Polish · Polished Outer Lip
Family 04

Special Finishes

Precision CNC diamond-cut face turning, multi-stage liquid metallics, and dark chrome/tinted clear combinations requiring multi-pass booth cycles.

Diamond Cut · Black Chrome · Hyper Silver
Family 05

2-Piece Paint Contrast

Independent finishing of the forged center disc, stepped outer lip, inner barrel, and perimeter assembly hardware on modular Duo-Block sets.

Contrast Center + Polished/Brushed Barrel

Compare curated GTRS finishes—including wheel-relief renders and macro surface textures—on the dedicated Finishes page.

Explore All Finishes

Release & Export Protocol

Pre-Shipment Quality Control & Protective Packing

Every bespoke wheel set undergoes a four-part release protocol between the finishing booth and courier dispatch so specification accuracy and surface condition are verified before international transport.

Check 01

Fitment & Specification Check

Diameter, width, offset, bolt pattern, center bore, construction, and finish checked against the order specification before release.

Dimensional & Order Verification
Check 02

Surface & Finish Check

Visual inspection of face, spoke windows, lip/barrel surfaces, bare-metal hub mounting pad, and center cap area before packing.

Full-Set Visual Inspection
Check 03

Pre-Shipment QC Media

Photo and video confirmation of the finished wheel set prepared on the inspection floor prior to export packing and dispatch.

Customer Order Documentation
Check 04

Individual Wheel Protection

Protective foam collars, outer rim lip guards, face covers, and heavy-wall export carton packing for international transport.

Export Transit Packaging

Configure Your Specification

Select Construction, Design, Diameter, and Finish

Move from the manufacturing sequence into the interactive GTRS Configurator or browse the full forged wheel collection across Monoblock, Deep Lip, Duo-Block, and Aero architectures.

Bespoke Fitment & Engineering Review

Discuss a Custom Build or Brake Clearance Requirement

Planning a staggered setup, big-brake kit clearance review, or two-piece Duo-Block specification? Connect directly with GTRS engineering for pre-order fitment consultation.